


 BUY NOW AND GET FREE SHIPPING
On all orders over 500,- (DK only)
 1-2 DELIVERY DAYS
Order before 12 noon and we will ship the same business day
 14 DAY RETURN RIGHT


Couldn't load pickup availability
17 in stock : 1-2 weekdays


Free shipping on orders over 500 DKK in DK

Ships from Roskilde DK

Local service center in Roskilde

1 year warranty

Customer Service
Email: hello@3dsaga.com
Phone: +45 69 15 31 11
All weekdays from 10:00 - 15:00
Showroom:
Monday - Thursday: 09:30 – 15:30
Friday: 09:30 – 15:00

Bambu Lab Support for ABS
Product Features
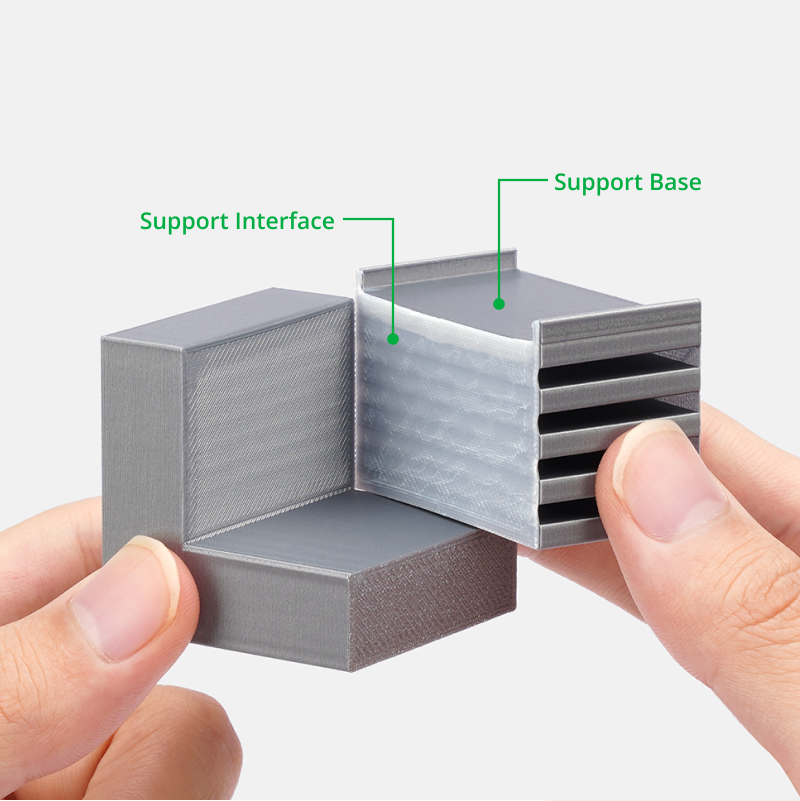
Easy support removal
Superior quality at the support interface
Comes with a reusable high-temperature spool
Diameter: 1.75 mm +/- 0.05 mm
Precautions for Use
For support use ONLY
Optional drying before use
Requires printer with a closed enclosure
Compatible with AMS 2 Pro, AMS HT, and AMS
AMS lite is NOT compatible
Note: Before printing, please refer to the print tips for optimal results.
Bambu Lab Support for ABS
Enhance your ABS printing experience with this innovative support material. Designed for seamless printing and easy removal, it ensures a flawless support interface every time. Fully compatible with the Bambu Lab AMS (Automatic Material System), streamlining your ABS printing process from start to finish.

Easy support removal
Specifically formulated for ABS, this support material adheres precisely to ABS surfaces, allowing for easy and clean removal. This reduces post-processing time and improves workflow efficiency.
Superior support interface quality
Support for ABS allows for a 0 Top Z distance and 0 Top interface spacing during printing, ensuring a mark-free support surface. This improves detail sharpness and the overall appearance and integrity of your finished prints.


RFID for intelligent printing
All print parameters are embedded in the RFID and can be automatically read by the AMS system. Load and print - no cumbersome manual setup.

Parameter comparison
Read more about different filament comparisons in the Bambu Filament Guide >>
| Parameter | Support for PLA/PETG | Support for PLA | Support for ABS | Support for PA/PET | PVA |
|---|---|---|---|---|---|
| Color | Natural | White & Black | White | Green | Clear |
| Nozzle Type | All sizes / materials | All sizes / materials | Hardened steel nozzle (Hotend) 0.4 mm / 0.6 mm / 0.8 mm | Stainless steel nozzle (Hotend) 0.4 mm | Hardened steel 0.4 mm / 0.6 mm (recommended) / 0.8 mm |
| Nozzle Temperature | 190–220 °C | 220–230 °C | 240–270 °C | 280–300 °C | 220–250 °C |
| Bed Temperature | 35–60 °C | 35–45 °C | 80–100 °C | 80–100 °C | 35–45 °C |
| Print Speed | < 100 mm/s | < 200 mm/s | < 100 mm/s | < 100 mm/s | < 200 mm/s |
| Solubility | Water-insoluble | Water-insoluble | Water-insoluble, limonene-soluble | Water-insoluble | Water-soluble |
| Drying Before Use | Optional | Optional | Optional | Required | Required |
| Dry Protection During Use | Optional | Optional | Optional | Required | Required |
| Filament Compatibility | PLA, PETG | PLA | ABS | PAHT-CF, PA6-CF, PA6-GF, PET-CF | PLA, PETG |
Accessory Compatibility
| Category | Recommended | Not Recommended |
|---|---|---|
| Build Plate | Smooth PEI Plate, Textured PEI Plate | Cool Plate SuperTack |
| Hotend | Hotend with hardened steel nozzle 0.4 mm / 0.6 mm / 0.8 mm Hotend with stainless steel nozzle 0.4 mm |
Hotend with hardened steel nozzle 0.2 mm Hotend with stainless steel nozzle 0.2 mm |
| Adhesive (Bambu Liquid Glue / Glue Stick) | Bambu Liquid Glue / Glue Stick | / |
Recommended Print Settings
| Parameter | Value |
|---|---|
| Drying Settings (Blast Drying Oven) | 80 °C, 4 hours |
| Humidity During Printing and Storage | < 20 % RH (sealed, with desiccant) |
| Nozzle Temperature | 240–270 °C |
| Bed Temperature (with adhesive) | 80–100 °C |
| Print Speed | < 100 mm/s |
Physical Properties
| Parameter | Value |
|---|---|
| Density | 1.16 g/cm³ |
| Vicat Softening Temperature | N/A |
| Heat Deflection Temperature | N/A |
| Melting Temperature | 195 °C |
| Melt Index | 11.6 ± 0.7 g/10 min |
Mechanical Properties
| Parameter | Value |
|---|---|
| Tensile Strength | N/A |
| Elongation at Break | N/A |
| Flexural Modulus | N/A |
| Flexural Strength | N/A |
| Impact Strength | N/A |
Downloads
Filament TDS
Filament MSDS
Filament RoHS
Print tips
• Support for ABS is soluble in limonene. Please be aware of proper usage and safety precautions.

• Strong and unpleasant odors may be released during printing. Make sure the printer is enclosed and placed in a well-ventilated area.
• When layer strength is important, it is recommended to increase the flush volume to over 800 mm³. Insufficient purging can reduce layer adhesion in the model on surfaces that are on the same horizontal plane as the support surface.
• Increasing the "initial layer speed" can result in easier-to-remove support. However, this increases the risk of warping.
• Dry the filament before use for higher print quality. Drying conditions: 80 °C for 4 hours in a hot air drying oven; 85–95 °C for 6 hours on the X1 series heated bed. Please refer to the filament drying guide on WIKI.
• For more support-related settings, please refer to Support on WIKI.
What's in the box
